


Pacific Lubrication Consultants supplies a comprehensive range of food grade oils for food processing and manufacturing equipment across Australia. Our range includes food grade gear oils, food grade hydraulic oils, food grade chain oils, food grade compressor oils and specialty oils.
Food manufacturing equipment operates under demanding conditions, including high and low temperatures, heavy loads, moisture, frequent washdowns and continuous production schedules. Using the correct lubricating oil helps protect critical components against friction, wear, corrosion and premature failure while supporting reliable equipment operation.
In areas where incidental contact with food may occur, lubricant selection also forms part of a facility's broader food safety program. Pacific Lubrication Consultants supplies H1 registered food grade lubricant solutions designed to combine food safety requirements with the performance needed by modern processing equipment.

Characteristics of Food Grade Oils
When you select fitting food grade lubricant for the application,
it will provide you with vital benefits such as:

Registered H1 Food Grade

Zinc-free and ash-less

Odourless

Low foaming

Wide application range

Endures heavy workloads
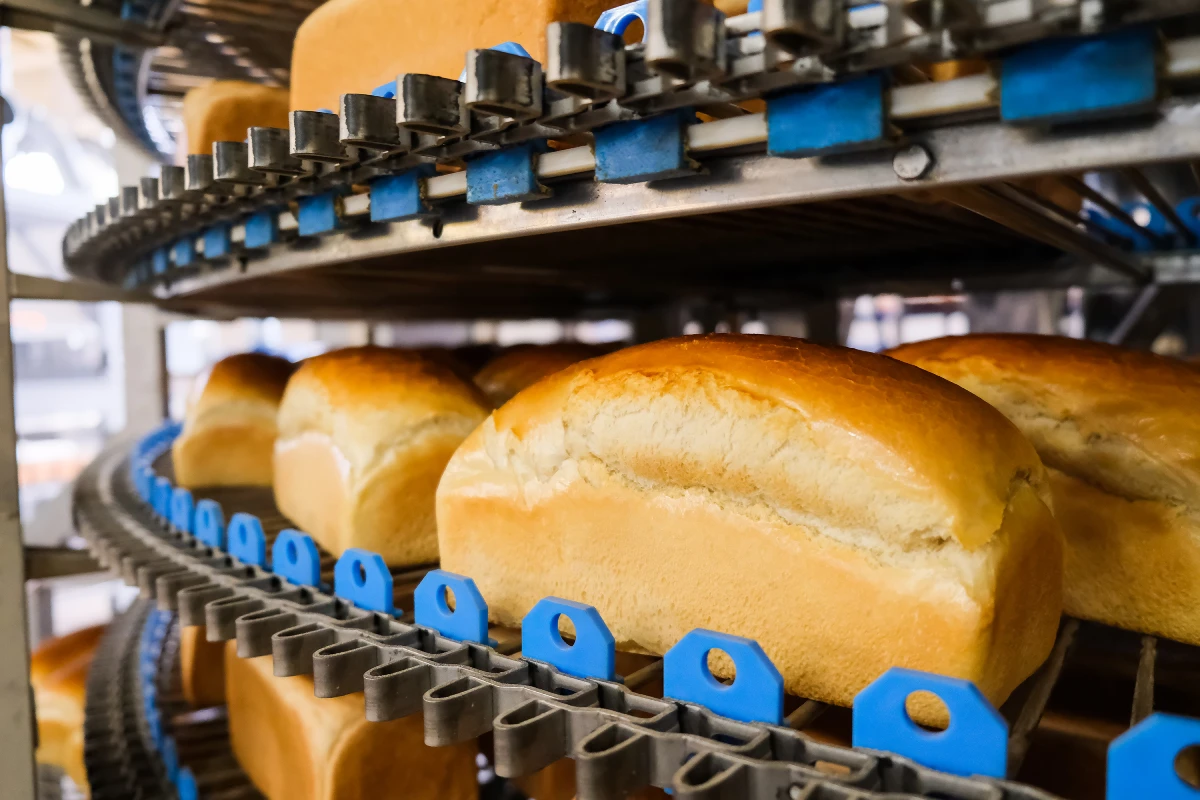
Food grade oils perform many of the same essential functions as conventional industrial lubricating oils, but they are formulated for use in environments where food safety is a key consideration. Different machinery and operating conditions require different oil properties, which makes correct lubricant selection important.
Common applications include:
- Gearboxes and transmissions: Food grade gear oils help reduce friction and wear between moving gear surfaces, particularly under demanding loads.
- Hydraulic systems: Food grade hydraulic oils provide lubrication while acting as the power transmission medium within hydraulic equipment.
- Chains and conveyors: Food grade chain oils provide lubrication for conveyor chains, oven chains, guides and sliding surfaces.
- Compressors and vacuum pumps: Suitable compressor oils help control wear, deposits and oxidation while protecting components such as seals and gaskets.
- Bearings and general machinery: Multipurpose and specialty oils can provide lubrication and corrosion protection across a range of food processing applications.
Matching the oil to the equipment, operating temperature, load and required viscosity can improve lubrication performance and help reduce avoidable maintenance.
About Synthetic Oils
Synthetic food grade oils are engineered to provide consistent lubrication performance across demanding operating conditions. Depending on the formulation and application, synthetic oils can provide advantages in areas such as oxidation stability, temperature performance and service life.
This can be particularly valuable in food manufacturing facilities where machinery operates continuously, at high temperatures or under significant loads.
High-quality synthetic lubricating oils may help reduce deposits and sludge formation, protect components against wear and support longer lubrication intervals. These properties can contribute to lower maintenance requirements, less unplanned downtime and more reliable equipment performance.

The benefits of using synthetic oils
When you select fitting food grade lubricant for the application,
it will provide you with vital benefits such as:

Uninterrupted production

Lower power consumption

Reduce running temperatures

Prolonged re-lubrication period

Lesser wear on parts

Lower cost of maintenance

Less downtime

Longer oil life


There is no single food grade oil suitable for every piece of machinery. The correct lubricant should be selected according to the equipment manufacturer's requirements and the conditions in which the machinery operates.
Important factors include:
- Required ISO viscosity grade
- Operating temperature range
- Equipment speed and load
- Water and washdown exposure
- Oxidation stability
- Corrosion and wear protection
- Compatibility with seals and gaskets
- Relubrication or oil change intervals
- Food safety and registration requirements
Viscosity is particularly important. An oil that is too thin may not provide an adequate lubricating film under the required load, while an oil that is too viscous can increase resistance and affect equipment efficiency.
Pacific Lubrication Consultants can assist food and beverage manufacturers in identifying appropriate lubricants for specific machinery and operating conditions.
Food Grade Oil and Food Safety Compliance
In food processing environments, lubricant management needs to consider both machinery reliability and contamination risk.
H1 lubricants are intended for applications where incidental food contact may occur. Third-party registration provides additional assurance that a lubricant meets recognised requirements for food grade applications.
Using clearly identified food grade oils can also support better lubricant management across a facility. Maintenance teams can establish appropriate lubrication procedures, reduce the risk of using an unsuitable lubricant and maintain documentation for food safety and maintenance programs.
Pacific Lubrication Consultants supplies H1 registered food grade lubricants and provides lubrication solutions, technical support and programs for food and beverage manufacturers across Australia.
Choosing a lubricant should not be based on food grade status alone. The oil must also perform its mechanical function effectively.
A correctly selected food grade oil can help:
- Reduce friction and component wear
- Protect against rust and corrosion
- Control oxidation and lubricant degradation
- Maintain reliable operation across changing temperatures
- Reduce lubricant-related equipment failures
- Extend oil and component service life
- Reduce unnecessary maintenance intervention
- Support consistent production and equipment uptime
This makes lubricant selection an important part of both preventive maintenance and food safety management.
Frequently Asked Questions About Food Grade Oils
What is food grade oil?
Food grade oil is a lubricant formulated for use in food and beverage processing environments. H1 registered lubricants are suitable for applications where incidental contact between the lubricant and food may potentially occur.
What is H1 food grade oil?
H1 is a classification for lubricants intended for applications where incidental food contact may occur during food manufacturing, processing or packaging.
Where are food grade oils used?
Food grade oils can be used in gearboxes, hydraulic systems, compressors, chains, conveyors, bearings, pumps and other food processing machinery. The appropriate lubricant depends on the equipment and its operating requirements.
Are synthetic food grade oils better than mineral oils?
Not necessarily for every application. Synthetic oils can provide advantages such as improved oxidation stability, temperature performance and longer service intervals in demanding applications. The correct choice should be based on equipment specifications and operating conditions.
How do I choose the correct food grade oil viscosity?
Always consider the equipment manufacturer's viscosity requirements together with operating temperature, speed and load. Pacific Lubrication Consultants can assist with selecting an appropriate food grade lubricant for specific equipment and operating environments.
Get In Touch with Pacific Lubrication Consultants
Need help selecting the right food grade oil for your equipment or food manufacturing facility? Call Pacific Lubrication Consultants on 1300 733 929 to discuss food grade oils, lubricant selection and lubrication solutions for your operation.
Get In TouchPacific Lubrication Consultants supply diverse food grade oils for various applications in the food manufacturing industry, including gear oils, hydraulic oils, chain oils, compressor oils and specialty oils.
These food grade oils are high-performance and are food-safe. They increase equipment reliability, help lower interruptions and avert pointless maintenance-related costs.
Characteristics of Food Grade Oils
When you select fitting food grade lubricant for the application,
it will provide you with vital benefits such as:
Registered H1 Food Grade
Zinc-free and ash-less
Odourless
Low foaming
Wide application range
Endures heavy workloads
About Synthetic Oils
Synthetic oils are made by man and are purified, distilled, refined and broken down through chemical engineering, improving their purity.
Synthetic oils have energy, thermal and performance advantages over mineral oils. Synthetic oils have superb oxidation stability at high temperatures, resulting in less carbon, acid or sludge accrual,
so it has a longer life.
The benefits of using synthetic oils
When you select fitting food grade lubricant for the application,
it will provide you with vital benefits such as:
Uninterrupted production
Lower power consumption
Reduce running temperatures
Prolonged re-lubrication period
Lesser wear on parts
Lower cost of maintenance
Less downtime
Longer oil life
Get In Touch with Pacific Lubrication Consultants
Call us at Pacific Lubrication Consultants on 1300 733 929 to enquire about food-grade oil or other lubricants.
Get In TouchPacific Lubrication Consultants supply food-grade greases from the trusted brand Cargo Oil. Our food-grade grease products include White Grease, Clear Grease, Open Gear Grease, White Anti-seize, ElectraFlow, O'ring, and Seal Lubricant. We supply H1-registered food-grade lubricants from the trusted brand Cargo Oil, which are used in the food-processing industry and involve possible incidental food contact in trace amounts. These food-grade greases are waterproof, can endure heavy workloads, provide powerful adhesion, are mechanically stable, water resistant, endures extreme environments, and has a wide range of uses.
Food Grade Greases are Used In the following Applications:
- Food processing industry
- All food production facilities
- All pharmaceutical facilities
- High-temperature applications
- Open Gears, Chains, Gearboxes (grease lubricated)
- Electrical terminals and switches
- Junction boxes and connections
- Hydraulic & pneumatic components
- O'rings and seals
- Hydrostatic cookers
- Chassis
- Bushings
- Saltwater contact
- Steam contact and more
Food-Grade Grease for Equipment
Food-grade greases are also used in various food-processing and industrial equipment applications. These include enclosed gearboxes, linkages and slides, joints, centralised lubrication systems and plain and rolling element bearings. Along with performing technical functions as any other lubricant, food-grade greases have other stringent requirements, such as:
- It remains physiologically nonreactive, nontoxic, harmless, tasteless and odourless.
- It withstands degradation from food products, water, steam and chemicals.
- It demonstrates a neutral behaviour when in contact with plastics and elastomers.
Get In Touch with Pacific Lubrication Consultants
If you need help selecting the food grade lubricant for your needs, our expert team is here to help you with the best advice and products. Feel free to call us at Pacific Lubrication Consultants on 1300 733 929, and we will be delighted to help you.
Get In TouchFood Grade Aerosol Sprays
Pacific Lubrication Consultants supply H1-registered food-grade aerosol sprays from the established brand Cargo Oil, perfect for food processing, manufacturing, and pharmaceutical applications. Our food-grade aerosol products include heavy-duty chain lube, multi-lube, Silicone Spray, Ultra Rust Release, Synlube, Super Stick and dry silicone spray. Food-grade aerosols products provide powerful adhesion, are water resistant, best for low maintenance applications, waterproof, general purpose lubricant, transparent, penetrates and have a wide range of uses.
Food Grade Aerosols are Ideal for the following Uses:
- Food processing industry
- Chains, gears, wheels, cogs and sprockets
- Plastic moulding release agent
- A broad range of lubrication applications
- Loosens rusted nuts and bolts
- Penetrates and frees rusted and corroded chains
- Forklift chains
- Wire cables
- Sliding surfaces and more
Get In Touch with Pacific Lubrication Consultants
If you need help selecting the food grade lubricant for your needs, our expert team is here to help you with the best advice and products. Feel free to call us at Pacific Lubrication Consultants on 1300 733 929, and we will be delighted to help you.
Get In Touch
We have been designing and installing lubrication systems since 1994, and as an Australian approved reseller and service agent for Lincoln / SKF lubrication systems with factory experience, there is no lubrication system we can’t handle. Please contact us for more info.
Connect With Us
We’d love to hear from you.


